-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (652)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (426)
-
Anaerobic Digester (202)
-
Industrial Water Tanks (349)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1722)
-
Double Membrane Roof (223)

|
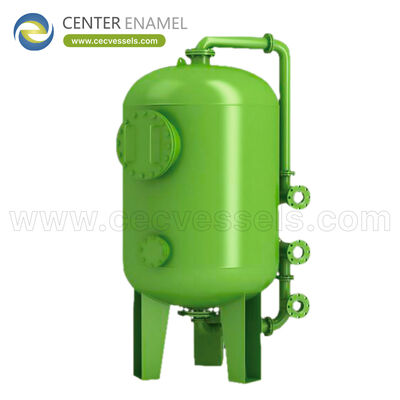
China Well Testing Separator Manufacturer Providing Accurate Multi Phase Separation Solutions For Oilfield Evaluation Applications
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
China Well Testing Separator Manufacturer Providing Accurate Multi Phase Separation Solutions For Oilfield Evaluation Applications
A well testing separator is used during well evaluation to separate the test stream and measure oil, gas, and water rates so engineers can judge reservoir deliverability. Here, separation quality is not just an operations issue - it is the foundation of measurement accuracy.
This guide explains how separation quality drives test accuracy, the metering and test-method choices, and a specification checklist so buyers can request a separator that produces data they can trust.
Why Separation Quality Drives Test Accuracy
Well-test meters read each phase after separation. If liquid carries gas or water carries oil, every downstream measurement is biased. The well testing separator therefore exists to deliver clean, stable phase streams to the meters.
Poor separation inflates or hides rates and leads to wrong reserve and completion decisions. Selection targets measurement-grade separation, not just bulk splitting.
Test Methodology And Separator Role
A typical test flows wellstream into the separator, measures gas on the top line and liquid in a calibrated tank or Coriolis meter, then calculates ratios. The separator must hold stable levels and interface so the meter sees steady phases.
Transient or unstable separation produces noisy data; the vessel and controls should be specified for stability during the test window.
Metering And Measurement Choices
Gas is usually metered by orifice or turbine; liquid by tank gauging or Coriolis. The separator must present clean phase to each. Selection should state the metering concept so nozzles and internals support it.
Buyers often specify the separator without the meter interface, then discover the separator cannot deliver clean phase to the chosen meter. Co-specifying both avoids this.
Stability, Levels, And Interface Control
Test accuracy depends on steady liquid levels and a clean oil-water interface during metering. The vessel needs reliable level and interface control and enough retention for the expected cut. Short retention or poor control undermines the whole test.
Specify expected rates, GOR, water cut, and test duration so retention and control are matched to the evaluation plan.
Specification Checklist Before RFQ
Provide test-rate range, GOR, water cut, pressure, temperature, metering concept, and required measurement uncertainty. State code and any skid/mobility needs.
A qualified manufacturer returns a separator with internals and nozzles matched to the metering plan and the test envelope.
Separator Feature Vs Test Outcome
| Feature | Supports | If Missing |
| Clean phase split | Accurate metering | Biased rates |
| Stable levels | Steady measurement | Noisy data |
| Interface control | Correct water cut | Oil-in-water error |
| Retention | Settling time | Carryover |
| Nozzle layout | Meter coupling | Installation gap |
Well Testing Separator Selection Parameters
| Parameter | Specify | Reason |
| Test rate range | Min-max | Envelope sizing |
| GOR | scf/bbl | Gas capacity |
| Water cut | Percent | Interface design |
| Pressure / temp | Oper + design | Code, velocity |
| Metering | Concept | Nozzle match |
| Uncertainty | Target | Design to data need |
| Code | ASME / GB | Acceptance |
Procurement, Acceptance, And Lifecycle
For a separator order, procurement starts with a complete specification: duty, stream composition, pressure and temperature, material, design code, and required inspection. A supplier who returns a written thermal or mechanical design basis - not just a price - lets the buyer compare bids on equal ground and avoids costly rework after fabrication begins.
Order quantities are flexible, with a minimum order quantity of one unit, which supports both pilot and full-scale projects. Typical fabrication and inspection lead time is approximately two months from confirmed design and material release, so the purchaser should align the milestone with the overall project schedule and freeze the specification early.
Payment is commonly handled through L/C or T/T terms, and acceptance should be defined up front: material certificates, dimensional check, hydrostatic or pneumatic test, and any market-specific documentation. Confirming the exact scope of supply and spare parts avoids ambiguity at the factory acceptance stage.
After delivery, lifecycle value depends on accessible design and clear operating limits. Request cleaning and inspection guidance, defined nozzle and access points, and the material basis so the unit can be maintained through its service life rather than replaced prematurely.
Specification freeze: confirm duty, code, and material before fabrication to protect lead time.
Acceptance scope: material certs, dimensional check, pressure test, and export docs.
Commercial terms: flexible MOQ (minimum 1), L/C or T/T, ~2-month typical lead.
Lifecycle: request inspection access and maintenance guidance at order.
Standards, Codes, And Quality Assurance
Qualified Separator supply is built on recognized pressure-equipment codes. Fabrication is routinely performed to ASME VIII Div.1 and GB/T 150, with CE / PED marking available for the European market. For hydrogen or sour service, material selection follows NACE MR0175 / ISO 15156 so the wetted path resists the specific environmental mechanism rather than relying on generic corrosion allowances.
Quality management runs to ISO 9001, and the manufacturing workflow includes material traceability from mill certificate to finished vessel, followed by hydrostatic or pneumatic testing and dimensional verification. Welding procedures and inspector qualifications are documented so the delivered unit can be audited against the stated code and project specification.
Buyers should name the exact codes and any additional standards at request-for-quotation stage. Doing so keeps marking, documentation, and acceptance aligned with the destination market and removes the most common cause of late-stage rework.
Codes: ASME VIII Div.1 and GB/T 150; CE/PED on request.
Material integrity: NACE MR0175 / ISO 15156 for H2 or sour service.
Quality: ISO 9001, full material traceability, pressure testing.
Documentation: mill certs, WPS/PQR, test and inspection records.
Conclusion
A well testing separator is selected to deliver measurement-grade separation: clean phase streams, stable levels, and a controlled oil-water interface so meters read accurately. Size on the test-rate envelope and GOR, co-specify the metering concept, and state required uncertainty. A qualified manufacturer should return a vessel with internals and nozzles matched to your evaluation plan, not a generic test unit.
About The Manufacturer
The manufacturer builds well testing separators to ASME VIII Div.1 and GB/T 150, with demisters, interface control, and nozzle layouts matched to metering packages, plus material traceability and pressure testing. Skid and mobility options are quoted on request.
Confirm test envelope, metering concept, order quantity, lead time, and inspection scope before ordering.
Frequently Asked Questions (FAQ)
What is a well testing separator?
A separator used during well evaluation to split test stream and enable accurate oil, gas, and water measurement.
Why does separation affect test accuracy?
Meters read each phase after separation; poor separation biases every rate calculation.
What does a well test measure?
Oil, gas, and water rates to assess reservoir deliverability and completion performance.
How is gas metered in a test?
Typically orifice or turbine on the gas outlet after clean separation.
How is liquid metered?
By calibrated tank gauging or Coriolis meter on the clean liquid stream.
Why specify metering with the separator?
The separator must deliver clean phase to the chosen meter; co-specifying avoids a mismatch.
What causes noisy test data?
Unstable levels or poor separation; fixed by retention and level/interface control.
What is interface control for?
Keeping oil-water boundary stable so water cut is measured correctly.
How is a test separator sized?
On test-rate envelope, GOR, water cut, and retention needed for settling.
What design code applies?
ASME VIII Div.1 or GB/T 150, named in the RFQ.
What uncertainty should I state?
Your required measurement tolerance so the vessel is designed to the data need.
Are skid/mobile options available?
Often yes; state mobility needs so the design includes handling features.
What causes biased rates?
Liquid in gas or oil in water from inadequate separation before metering.
What inspection should I require?
Hydrostatic/pneumatic test, material certs, and any market documentation.
How do I compare test separator bids?
On test envelope, metering match, code, and inspection - not price alone.
Suggested CTA: Send your test envelope and metering concept for an accurate well testing separator: Request Technical Specifications or Discuss Your Project.