-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (660)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (505)
-
Anaerobic Digester (217)
-
Industrial Water Tanks (404)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1852)
-
Double Membrane Roof (223)
|
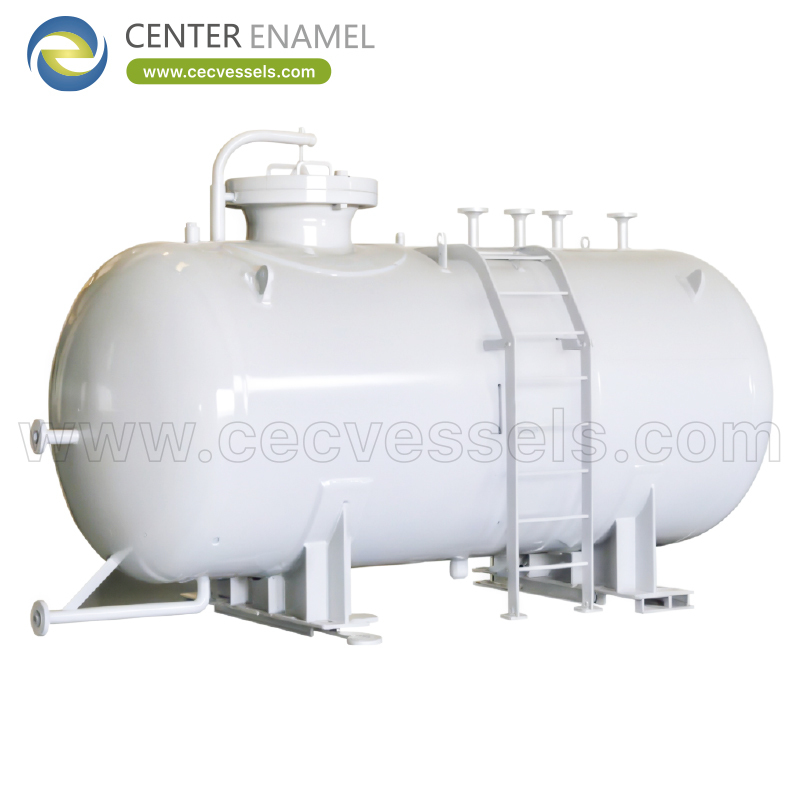
Pressure Vessel Welding Procedures Joints And NDT
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
Pressure Vessel Welding Procedures Joints And NDT
Pressure vessel welding is a code-controlled activity, not just a shop operation: each seam is made to a qualified procedure, by a qualified welder, and is examined by a method matched to the flaw it might contain.
This guide covers procedure qualification, process and joint selection, consumables, distortion control and the NDT methods that turn a welded seam into verifiable evidence.
Welding Is A Code Activity
The pressure boundary is only as strong as its welds, so codes require that welding be performed to a written procedure that has been qualified by testing. The qualification demonstrates that the proposed parameters produce sound, property-compliant joints.
This is why a vessel data book contains a weld map, welding procedure specifications and welder qualifications alongside the NDT reports. A visually neat weld without this paperwork is not a code weld.
Welding Process Selection
Shielded metal arc welding is versatile for short seams and repair; gas tungsten arc welding gives a clean, controlled root pass; submerged arc welding is efficient for long longitudinal and circumferential seams in a controlled position.
The choice follows joint geometry, position, material and productivity. A common approach is a GTAW root for quality followed by SAW fill on long seams, balancing root integrity with deposition rate.
WPS And PQR Qualification
A Welding Procedure Specification states the variables - process, base metal group, filler, current, voltage, travel speed, preheat and post-heat. A Procedure Qualification Record supports it with the results of a test weld and the mechanical tests performed on it.
The PQR defines the range within which the WPS remains valid. Changing an essential variable outside that range requires a new qualification, so procedure control is a live part of fabrication, not a one-time document.
Joint Design And Weld Bevels
Pressure seams are generally full-penetration butt joints; the bevel - V, U or X - is chosen for thickness and access, and a backing bar or back-gouge is used to achieve a clean root from both sides.
Joint access matters for inspection as well as welding. A design that leaves a seam inaccessible for radiography or ultrasonic scanning creates an examination gap that must be resolved before fabrication.
Welding Consumables And Matching
Filler metal is selected to match the base material's strength and corrosion behaviour, with low-hydrogen consumables used where hydrogen cracking is a concern. Consumable storage and handling are controlled because moisture pickup can introduce hydrogen into the weld.
For stainless and duplex grades, filler choice also controls ferrite content and corrosion resistance; the specification should name the consumable class, not leave it to shop preference.
Distortion And Sequence Control
Welding shrinks as it cools, and an uncontrolled sequence can bow a shell course or pull a nozzle out of alignment. Balanced welding, back-stepping and controlled interpass temperature reduce both distortion and residual stress.
Fit-up quality is part of this control: excessive root gap or high-low misalignment concentrates stress and makes a sound weld much harder to achieve, regardless of the procedure used.
NDT Methods And Acceptance
Radiography and ultrasonics detect internal discontinuities such as porosity, slag or lack of fusion; magnetic particle and liquid penetrant detect surface and near-surface cracks; visual and dimensional checks apply to every weld.
Each method has a defined acceptance standard under the governing code. The inspection plan states which seams get which method and to what extent - full or spot - because that choice also sets the joint efficiency used in design.
Weld Documentation And Traceability
A weld map numbers every seam and links it to the WPS used, the welder, the NDT result and any repair. This record is the thread that lets an inspector reconstruct how the boundary was made.
Repairs are logged with their cause and re-examination result. A cluster of repairs on one seam type is a useful signal that the procedure, fit-up or operator needs review rather than repeated local patching.
NDT Method By Flaw Type
Method |
Detects |
Typical use |
Radiography (RT) |
Internal porosity / slag |
Butt seams |
Ultrasonic (UT) |
Internal lack of fusion |
Thick seams |
Magnetic particle (MT) |
Surface cracks, ferro magnetic |
CS surfaces |
Penetrant (PT) |
Surface cracks, non-magnetic |
SS surfaces |
Welding Control Inputs
Input |
Why it matters |
Base material group |
Sets WPS / PQR range |
Joint type / thickness |
Sets bevel and process |
Filler class |
Strength / corrosion match |
Examination extent |
Sets joint efficiency |
Preheat / PWHT |
Crack and stress control |
Weld map |
Traceability of seams |
Acceptance code |
Defines pass / fail |
Conclusion
Pressure vessel welding quality comes from control, not appearance: a qualified WPS backed by a PQR, a sensible process and joint design, controlled consumables and a sequence that limits distortion.
Match the NDT method to the likely flaw and put the full weld map in the data book; when reviewing a supplier, ask to see the procedure qualification and a completed weld map, not only photographs of neat seams.
About Center Enamel
Center Enamel is a pressure vessel and process equipment manufacturer based in China, producing stainless steel and carbon steel pressure vessels, separators, reactors, heat exchangers and storage tanks for chemical, oil and gas, power, food, pharmaceutical and water-treatment applications.
Fabrication is carried out under ASME VIII Div.1, GB/T 150 and ISO 9001 with CE/PED and NACE MR0175 / ISO 15156 options for sour service. Each unit is supplied with material traceability, documented welding procedures, NDT, hydrostatic testing and an export data book.
- Material range: Stainless steel (304 / 316L), duplex and carbon steel with rubber or epoxy lining for corrosion duty.
- Standards: ASME VIII Div.1, GB/T 150, ISO 9001, CE/PED, NACE MR0175 / ISO 15156.
- Commercial terms: Minimum order quantity 1 unit, typical lead time about 2 months, L/C or T/T.
Frequently Asked Questions (FAQ)
What is pressure vessel welding?
Code-controlled joining of the pressure boundary using qualified procedures, qualified welders and inspection methods matched to the seam.
What is a WPS?
A Welding Procedure Specification listing the variables - process, materials, filler, current, preheat - under which a production weld must be made.
What is a PQR?
A Procedure Qualification Record: the test weld results and mechanical tests that prove a WPS can produce acceptable joints.
Which welding processes are common?
SMAW for general and repair work, GTAW for controlled root passes and SAW for long, position-controlled shell seams.
Why use a GTAW root?
It gives a clean, well-controlled root, which is the most defect-prone part of a full-penetration butt weld.
What is joint efficiency?
A design factor linked to the extent of weld examination; more examination permits a higher efficiency and thinner shell.
What does full penetration mean?
The weld fuses through the full joint thickness, unlike a fillet weld; pressure seams are normally full penetration.
Why control consumable storage?
Moisture in low-hydrogen consumables can introduce hydrogen into the weld and cause cracking; controlled storage prevents this.
How is distortion limited?
Through balanced sequencing, back-stepping, correct root gap and alignment, and controlled interpass temperature.
Which NDT finds surface cracks?
Magnetic particle testing on ferromagnetic carbon steel and liquid penetrant testing on stainless and non-magnetic materials.
Which NDT finds internal flaws?
Radiography and ultrasonics detect internal porosity, slag, lack of fusion and similar discontinuities.
What is a weld map?
A numbered drawing linking each seam to its WPS, welder, NDT result and any repair history.
Are repairs acceptable?
Yes when made to a qualified repair procedure and re-examined; every repair is recorded in the weld map.
Does a neat weld mean a good weld?
No. Acceptance depends on examination results and documentation, not appearance alone.
What should a buyer request?
A sample WPS/PQR, the weld map from a comparable vessel and the NDT acceptance standard the shop applies.
Suggested CTA: Request a technical quotation with your duty, pressure, temperature and fluid data, or discuss your vessel specification with a Center Enamel engineer for a sized proposal.