-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (660)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (505)
-
Anaerobic Digester (217)
-
Industrial Water Tanks (404)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1852)
-
Double Membrane Roof (223)
|
Pressure Vessel Shell Thickness Forming And Tolerances
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
Pressure Vessel Shell Thickness Forming And Tolerances
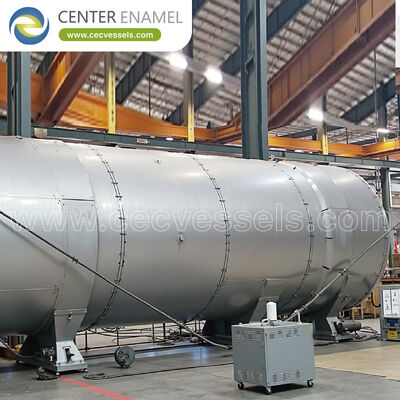
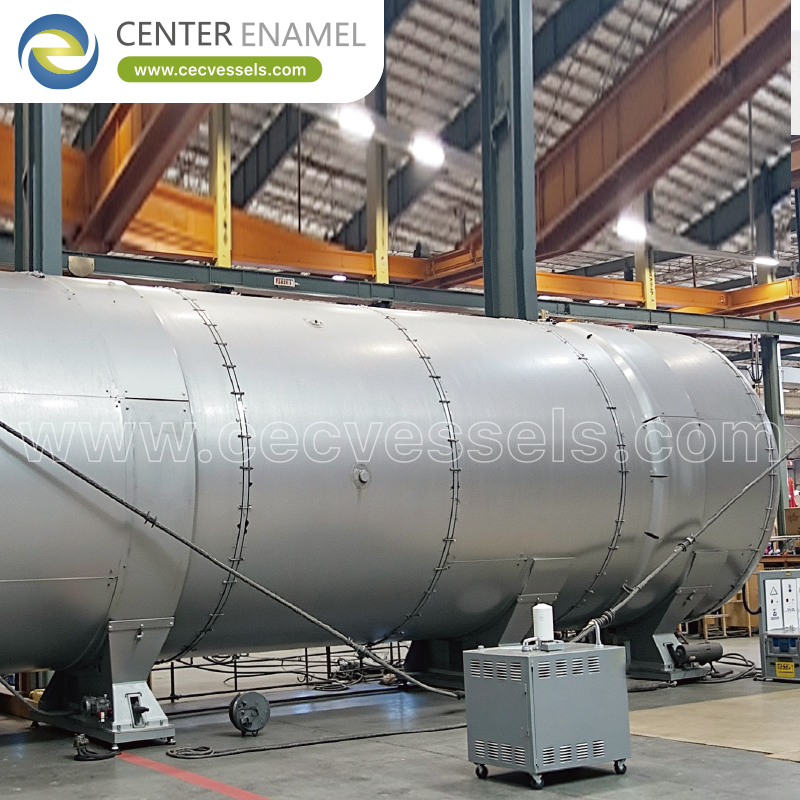
The pressure vessel shell is the main cylindrical boundary carrying internal pressure and often external loads as well. Its thickness, roundness and seam layout decide whether the vessel meets both its pressure rating and its fit-up tolerances.
This guide covers required versus nominal thickness, course construction, rolling methods, ovality and seam design, with the dimensional checks that release a shell for assembly.
The Shell Is The Main Boundary
In most vessels the cylindrical shell contains the largest pressure-loaded area and therefore dominates material mass. It also carries liquid static head, wind, seismic and support loads, so its design is rarely governed by pressure alone.
The shell is built from one or more rolled courses joined by longitudinal and circumferential welds. How those courses are arranged affects both stress and how efficiently the vessel can be fabricated.
Required Versus Nominal Thickness
The code calculation produces a required thickness for the governing load case. To that value the designer adds corrosion allowance and accounts for the permitted negative tolerance of the plate, then selects the next available nominal plate thickness.
Confusing calculated thickness with ordered thickness is a common error: the plate on the rolling machine must be thick enough that the finished shell still exceeds the code minimum after tolerance and corrosion provision.
Shell Course Construction
A tall vessel is built from several shell courses stacked vertically. Thicker courses are placed lower where pressure and static head are highest, and thickness may step down toward the top to save material.
Course heights are chosen around available plate sizes, head dimensions and nozzle locations. A good layout avoids placing a circumferential seam through a nozzle opening or a highly stressed transition.
Plate Rolling Methods
Plates are rolled on three- or four-roll machines. The plate ends are pre-bent so the rolled course closes in a true circle rather than leaving a flat area near the longitudinal seam.
Rolling is done progressively, checking curvature as the plate forms. Over-rolling or under-rolling produces a course that will not close cleanly, leading to high-low misalignment at the seam that is difficult to correct later.
Ovality And Dimensional Tolerances
No rolled shell is a perfect cylinder. Codes limit out-of-roundness, often expressed as the difference between maximum and minimum measured diameter, because ovality affects both pressure capacity under external load and the fit of internal parts.
Circumference, straightness and course height are also measured. These checks are made before assembly, when a re-rolling pass is still possible, rather than after the courses are welded together.
Longitudinal And Circumferential Seams
The longitudinal seam runs along the course axis and carries roughly twice the hoop stress of a circumferential seam in a thin cylinder, so it usually attracts the higher joint efficiency and more examination.
For that reason longitudinal seams are staggered between adjacent courses and kept clear of openings. Circumferential seams join courses and heads and are examined to the extent the design assigns them.
Forming Strain And Material Properties
Cold rolling strains the plate and can raise strength while reducing ductility at the formed zone. For some grades and thicknesses this changes properties enough that a forming or post-weld heat treatment is required.
The fabrication route should state when property restoration is needed, based on the material specification and code, rather than assuming that all rolled plate remains unchanged.
Shell Inspection Before Assembly
Before courses are joined, thickness is mapped, geometry measured and edges inspected for lamination or defects. Material marking is verified so each course can be traced to its certificate after cutting and rolling.
Releasing a shell course only after these checks prevents the costly situation where a defect or out-of-tolerance condition is discovered after welding has locked the geometry in place.
Shell Seam By Stress
Seam |
Stress |
Typical examination |
Longitudinal |
Higher (hoop) |
Full RT / UT commonly |
Circumferential |
About half |
Per code / design |
Head to shell |
Discontinuity |
Per code / design |
Nozzle to shell |
Local |
MT / PT + RT / UT |
Shell Design And Build Inputs
Input |
Why it matters |
Design pressure / load case |
Sets required thickness |
Corrosion allowance |
Added to required thickness |
Plate negative tolerance |
Raises ordered thickness |
Diameter / course height |
Sets rolling plan |
Joint efficiency |
Sets examination extent |
External pressure |
May govern thickness |
Dimensional tolerance |
Sets acceptance |
Conclusion
The pressure vessel shell is defined by more than a thickness number: nominal plate must survive tolerance, corrosion and forming, while roundness and seam layout govern whether the vessel can be assembled and inspected as designed.
Review the thickness basis and the dimensional acceptance criteria together, and confirm longitudinal seams are staggered and examined to the efficiency the calculation assumed.
About Center Enamel
Center Enamel is a pressure vessel and process equipment manufacturer based in China, producing stainless steel and carbon steel pressure vessels, separators, reactors, heat exchangers and storage tanks for chemical, oil and gas, power, food, pharmaceutical and water-treatment applications.
Fabrication is carried out under ASME VIII Div.1, GB/T 150 and ISO 9001 with CE/PED and NACE MR0175 / ISO 15156 options for sour service. Each unit is supplied with material traceability, documented welding procedures, NDT, hydrostatic testing and an export data book.
- Material range: Stainless steel (304 / 316L), duplex and carbon steel with rubber or epoxy lining for corrosion duty.
- Standards: ASME VIII Div.1, GB/T 150, ISO 9001, CE/PED, NACE MR0175 / ISO 15156.
- Commercial terms: Minimum order quantity 1 unit, typical lead time about 2 months, L/C or T/T.
Frequently Asked Questions (FAQ)
What is a pressure vessel shell?
The cylindrical pressure boundary of a vessel, built from one or more rolled plate courses and joined by longitudinal and circumferential welds.
What is required thickness?
The minimum thickness from the code calculation; corrosion allowance and plate tolerance are added before choosing nominal plate.
Why add corrosion allowance?
To compensate for expected wall loss in service; it is a design provision, not a guarantee of service life.
What is plate negative tolerance?
The permitted amount by which delivered plate may be under its nominal thickness, which must be allowed for when ordering.
Why are thicker courses at the bottom?
Because pressure plus liquid static head makes lower courses more highly loaded in a tall vertical vessel.
How are shell plates rolled?
On three- or four-roll machines with pre-bent ends so the course closes into a true circle.
What is ovality?
Out-of-roundness of a rolled shell, limited by code because it affects strength under external pressure and fit-up.
Which seam carries more stress?
The longitudinal seam, which in a thin cylinder carries roughly twice the stress of a circumferential seam.
Why stagger longitudinal seams?
To avoid aligning high-stress seams of adjacent courses and to keep them clear of openings.
Can the shell be too thin after rolling?
Yes if forming thinning or plate tolerance was not allowed for; thickness is mapped before assembly to confirm compliance.
Does cold rolling change material?
It strains and can strengthen the plate while lowering ductility; some grades need property-restoring heat treatment.
When is thickness stepped down?
When upper courses carry less pressure and static head, reducing plate thickness there saves material.
What is high-low misalignment?
A step across a weld from poorly matched course edges, which raises local stress and complicates examination.
What checks release a shell course?
Thickness mapping, diameter and ovality measurement, straightness and edge inspection with marking verification.
What should a buyer review on shell design?
The thickness basis, joint efficiency, external-pressure check and the dimensional acceptance criteria.
Suggested CTA: Request a technical quotation with your duty, pressure, temperature and fluid data, or discuss your vessel specification with a Center Enamel engineer for a sized proposal.