-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (660)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (485)
-
Anaerobic Digester (217)
-
Industrial Water Tanks (384)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1832)
-
Double Membrane Roof (223)
|
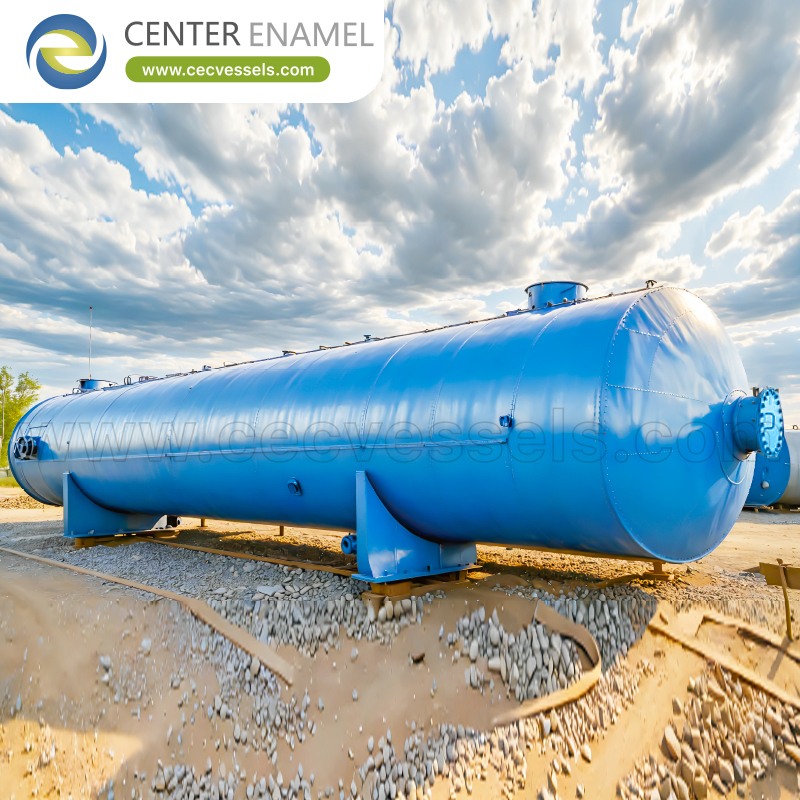
Pharmaceutical Pressure Vessel Hygienic Design GMP And Electropolished Construction
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
A pharmaceutical pressure vessel is judged less by pressure alone and more by cleanliness: it must resist product contact contamination, clean fully, and validate consistently under GMP.
That shifts the specification from wall thickness toward surface finish, drainage, sterile service and documented validation - the topics this guide covers, using verified material and code facts rather than assumed performance.
GMP Drives The Whole DesignGood Manufacturing Practice means the vessel must be designed, built and documented so product contact stays controlled and inspectable. Surfaces, joints and cleanability are qualification criteria, not afterthoughts.
Unlike a chemical shell where corrosion is the main limit, a pharma vessel is also failed by dead legs, poor drainage and surfaces that harbour residue - so the design answers both pressure and hygiene.
Material: 316L And ElectropolishPharmaceutical contact surfaces are typically 316L stainless for corrosion resistance and low extractables, finished by electropolishing to a smooth, low-roughness surface that resists adhesion and cleans readily.
Electropolishing also passivates the surface and reduces particle shedding; the finish target (often Ra 0.8 micrometre or better for contact areas) is a specification item, not a shop default.
Hygienic Geometry: No Dead LegsHygienic design eliminates dead legs, crevices and hard-to-clean corners; connections use sanitary fittings, and internal welds are full-penetration and dressed flush so product has nowhere to stagnate.
Drainage is designed in: the vessel and its nozzles slope to complete, verifiable drain-out so cleaning cycles leave no pooled residue that could later contaminate a batch.
Clean-In-Place And Sterile ServiceMost pharma vessels support CIP (clean-in-place) and often SIP (sterilise-in-place), with spray balls, cipered returns and sterile barriers integrated into the pressure boundary rather than bolted on.
For sterile service the vessel must hold its integrity through repeated thermal cycles, so gaskets, seals and the pressure boundary are selected for both pressure and repeated sterilisation.
Validation And DocumentationPharma vessels are validated, not just built: material certificates, weld maps, surface-finish records, cleaning validation and IQ/OQ documentation form the package regulators and auditors expect.
The data book therefore extends beyond code conformity to include traceability of every contact surface and the evidence that the vessel cleans and drains as designed.
Code Basis And Pressure BoundaryThe pressure boundary still follows ASME VIII Div.1 or GB/T 150, with CE/PED for the EU; the hygienic layer sits inside that code shell, so both must be satisfied without compromising either.
This dual requirement is why pharma vessels cost more than a plain process shell of the same pressure - the finish, fittings and validation carry real work.
Differentiating From Food-Grade DutyFood-grade vessels share the stainless and cleanable theme but pharma adds GMP validation, stricter extractables control and sterile-service readiness that food duty does not always require.
Specify to the higher bar when the product is injectable or high-potency; food-grade finish alone will not satisfy a pharma audit.
Procurement Checklist For PharmaRequire the contact material and finish in the PO, the sanitary fitting standard, CIP/SIP provisions, and the validation package; verify a sample data book that includes surface-finish and weld-map records.
Confirm the builder can deliver the hygienic layer - electropolish, dressed welds, drainable geometry - not just a code shell with a 'sanitary' label.
Pharma Versus Food-Grade VesselAspect |
Pharma |
Food-grade |
Standard |
GMP / cGMP |
3-A / EHEDG |
Validation |
IQ/OQ required |
Often lighter |
Extractables |
Strict control |
Organoleptic |
Sterile service |
Common (SIP) |
Less common |
Finish |
Electropolish Ra<=0.8 |
Polished, cleanable |
Input |
Why it matters |
Contact material |
316L, low extractables |
Surface finish |
Electropolish Ra target |
Drainage / dead legs |
Cleanability |
CIP / SIP |
Sterile service |
Validation pkg |
GMP evidence |
Code + marking |
Pressure approval |
A pharmaceutical pressure vessel is specified for GMP as much as for pressure: 316L contact surfaces, electropolished finish, drainable geometry and a validation package that proves cleanability and integrity.
Treat the hygienic layer and the code shell as two requirements that must both be met, and verify a sample data book that includes surface-finish and weld-map records before award.
About Center EnamelCenter Enamel is a pressure vessel and process equipment manufacturer based in China, producing stainless steel and carbon steel pressure vessels, separators, reactors, heat exchangers and storage tanks for chemical, oil and gas, power, food, pharmaceutical and water-treatment applications.
Manufacturing is carried out under ASME VIII Div.1, GB/T 150 and ISO 9001 with CE/PED and NACE MR0175 / ISO 15156 options for sour service. Each unit is supplied with material traceability, hydrostatic or pneumatic testing, NDT and export documentation.
- Material range: Stainless steel (304 / 316L), duplex, carbon steel with rubber or epoxy lining for corrosion duty.
- Standards: ASME VIII Div.1, GB/T 150, ISO 9001, CE/PED, NACE MR0175 / ISO 15156.
- Commercial terms: Minimum order quantity 1 unit, typical lead time about 2 months, L/C or T/T.
Hygienic design for GMP: 316L contact surfaces, electropolished finish, no dead legs, drainable geometry and a validation package.
Why 316L for pharma?Good corrosion resistance and low extractables for product contact; it is the common choice where purity and cleanability matter.
What does electropolishing do?Smooths and passivates the surface to a low roughness (often Ra 0.8 micrometre or better) that resists adhesion and cleans readily.
What is a dead leg and why avoid it?A stagnant pocket where product or cleaning fluid traps; hygienic design eliminates dead legs so the vessel drains and cleans fully.
What is CIP and SIP?Clean-in-place and sterilise-in-place; the vessel integrates spray balls and sterile barriers so it can be cleaned or sterilised without disassembly.
How is a pharma vessel validated?Through IQ/OQ and cleaning validation with material certs, weld maps, surface-finish records and a data book extending beyond code conformity.
Which code applies?The pressure boundary follows ASME VIII Div.1 or GB/T 150, with CE/PED for the EU; the hygienic layer sits inside that shell.
How is pharma different from food-grade?Pharma adds GMP validation, stricter extractables control and sterile-service readiness that food duty does not always require.
What finish is typical?Electropolished 316L contact surfaces, often Ra 0.8 micrometre or better for product-contact areas.
Are sanitary fittings needed?Yes; connections use sanitary fittings and full-penetration dressed welds so there are no crevices to harbour residue.
What documents prove pharma compliance?Material certs, weld maps, surface-finish records, cleaning validation and IQ/OQ, plus the code data report.
Why do pharma vessels cost more?The finish, sanitary fittings, CIP/SIP integration and validation package carry real work beyond a plain code shell.
Can a food-grade vessel serve pharma?Only if it meets the higher GMP bar; food-grade finish alone will not satisfy a pharma audit for injectable or high-potency product.
How long to fabricate?About 2 months from a China manufacturer for an engineered hygienic vessel scheduled around certification and finish.
What should the PO state?Contact material and finish, sanitary fitting standard, CIP/SIP provisions, validation package and the required code marking.
Suggested CTA: Request a technical quotation with your duty, pressure, temperature and fluid data, or discuss your project with a Center Enamel engineer for a sized proposal.