-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (660)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (475)
-
Anaerobic Digester (217)
-
Industrial Water Tanks (374)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1822)
-
Double Membrane Roof (223)

|
Pressure Vessel Factory Audit What To Verify On Site Before You Award
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
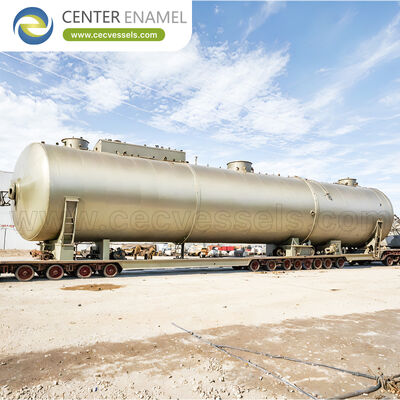
Pressure Vessel Factory Audit What To Verify On Site Before You Award
A pressure vessel factory audit is the on-site verification that turns a supplier's claims into evidence: it confirms the shop can actually design, weld, examine and stamp the vessel it quoted.
The efficient audit covers certifications and quality system first, then welding and NDE capability, then test facilities and traceability - and it is best done before award, when you can still walk away.
Certifications And Authorization On The Wall
Start with the ASME authorization, stamp scope and ISO 9001 certificate displayed and current; verify the scope covers your vessel class and pressure.
Check that the authorized inspector arrangement is active, because a lapsed AI relationship blocks U-Stamp sign-off regardless of the shop's skill.
Welding Procedure And Welder Qualification
Review the WPS/PQR library and confirm procedures exist for the actual joint types, materials and positions your vessel needs.
Verify welder qualification records are current and cover the processes used; expired qualifications are a frequent audit finding.
NDE And Examination Capability
Confirm the shop can perform or control radiography, ultrasonic, magnetic particle and dye-penetrant examination to the code and ITP requirement.
For critical seams, ask whether NDE is in-house or subcontracted and how results are recorded and linked to the vessel.
Test And Heat-Treatment Facilities
Inspect the hydrostatic/pneumatic test bay, pressure gauges with valid calibration, and any post-weld heat-treatment furnace for thick sections.
A shop that must outsource every test loses control of schedule and evidence, raising both risk and lead time.
Material Receiving And Traceability
Walk the receiving and storage area: are mill certificates matched to material, and is positive identification maintained from plate to fabricated part?
Traceability breaks down when certificates are filed separately from stock; verify the link is maintained on the shop floor.
Crane, Rolling And Dimensional Capacity
Confirm crane capacity, plate-rolling width and thickness, and head-forming capability against your vessel's dimensions and weight.
These physical limits decide whether your vessel is buildable here at all, independent of paperwork.
Documentation And Data-Book Practice
Ask to see a recently closed vessel's data book: material certs, WPS/PQR, NDT, heat-treatment charts and test certificate in one coherent file.
A clean, complete data book is the single best predictor of a smooth acceptance at your site.
Red Flags That Should Stop An Award
Block award on expired qualifications, no AI arrangement, no NDE control, broken traceability, or inability to show a complete recent data book.
These are not minor gaps; they indicate the shop cannot deliver a verifiable code vessel even if the quote looks attractive.
Pre-Award Versus Surveillance Audit
A pre-award audit judges capability and is best done before contract; a surveillance audit during fabrication confirms the shop is following what it claimed.
For critical or first-time suppliers, schedule a surveillance visit at the radiographic examination and hydrostatic test hold points so the key evidence is witnessed, not just certified later.
The two audits are complementary: one proves the shop can build the vessel, the other proves it is building your vessel to that standard.
Audit Focus Areas
| Area | What to verify | Deal-breaker if missing |
|---|---|---|
| Certification | ASME scope, ISO 9001, AI active | Yes |
| Welding | WPS/PQR, welder quals | Yes |
| NDE | RT/UT/MT/PT control | Yes |
| Test | Hydro bay, calibrated gauges | Usually |
| Traceability | Cert-to-part link | Yes |
Factory Capability Red Flags
| Red flag | Why it matters |
|---|---|
| Expired welder quals | Joints may be unqualified |
| No active AI | U-Stamp cannot be signed |
| NDE outsourced, uncontrolled | Results not linked |
| Broken traceability | Conformity unverifiable |
| No recent data book | Documentation weak |
Conclusion
A factory audit converts claims into evidence across certification, welding, NDE, test, traceability and documentation - and is best done before award while you can still walk away.
Treat expired qualifications, a missing AI arrangement, uncontrolled NDE or broken traceability as deal-breakers, because they mean the shop cannot deliver a verifiable code vessel.
About Center Enamel
Center Enamel is a pressure vessel and process equipment manufacturer based in China, producing stainless steel and carbon steel pressure vessels, separators, reactors, heat exchangers and storage tanks for chemical, oil and gas, power, food, pharmaceutical and water-treatment applications.
Manufacturing is carried out under ASME VIII Div.1, GB/T 150 and ISO 9001 with CE/PED and NACE MR0175 / ISO 15156 options for sour service. Each unit is supplied with material traceability, hydrostatic or pneumatic testing, NDT and export documentation.
- Material range: Stainless steel (304 / 316L), duplex, carbon steel with rubber or epoxy lining for corrosion duty.
- Standards: ASME VIII Div.1, GB/T 150, ISO 9001, CE/PED, NACE MR0175 / ISO 15156.
- Commercial terms: Minimum order quantity 1 unit, typical lead time about 2 months, L/C or T/T.
Frequently Asked Questions (FAQ)
What is a pressure vessel factory audit?
An on-site verification of a shop's ability to design, weld, examine and stamp the vessel it quoted, ideally before award.
What should I check first?
Certifications and stamp scope, then the active authorized-inspector arrangement, because a lapsed AI blocks U-Stamp sign-off.
Why review WPS/PQR?
To confirm procedures exist for your actual joint types, materials and positions, and that welder qualifications are current.
What NDE should the shop control?
Radiography, ultrasonic, magnetic particle and dye-penetrant examination to code, with results linked to the vessel.
Why visit the test bay?
To confirm a working hydrostatic/pneumatic bay, calibrated gauges and heat-treatment furnace for thick sections.
How is traceability verified?
By matching mill certificates to material on the shop floor and confirming positive identification from plate to part.
What physical limits matter?
Crane capacity, plate-rolling width/thickness and head-forming capability versus your vessel's size and weight.
What is a data book?
The complete file of certs, WPS/PQR, NDT, heat-treatment and test records for a finished vessel.
Which findings are deal-breakers?
Expired quals, no active AI, uncontrolled NDE, broken traceability, no recent complete data book.
Should I audit before or after award?
Before award, while you can still select another shop without penalty.
Can a small shop pass audit?
Yes, if it holds the right scope and quality system; facility size is secondary to authorization and discipline.
How long does an audit take?
Typically one to two days on site plus document review, depending on scope.
Do I need a third party to audit?
Not required, but a third-party inspector adds independence for high-risk or regulated duty.
What if NDE is subcontracted?
Acceptable only if the shop controls and records it and links results to the vessel.
Why is the data book the best predictor?
A clean, complete data book shows the documentation discipline that drives smooth site acceptance.
Suggested CTA: Request a technical quotation with your duty, pressure, temperature and fluid data, or discuss your project with a Center Enamel engineer for a sized proposal.