-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (660)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (485)
-
Anaerobic Digester (217)
-
Industrial Water Tanks (384)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1832)
-
Double Membrane Roof (223)

|
Practical Biogas Plant Design for Converting POME into Biogas in Honduras
| Place of Origin: | China |
| Brand Name: | CEC TANKS |
| Certification: | ISO 9001:2008, AWWA D103 , OSHA , BSCI |
| Model Number: | W |
| Minimum Order Quantity: | 1set |
| Price: | $5000~$20000 one set |
| Packaging Details: | PE poly-foam between each two steel plates ; wooden pallet and wooden |
| Delivery Time: | 10-30 days after deposit received |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 60 sets per month |
|
Detail Information |
|||
| Place of Origin | China | Brand Name | CEC TANKS |
|---|---|---|---|
| Certification | ISO 9001:2008, AWWA D103 , OSHA , BSCI | Model Number | W |
| Tank Body Color: | Dark Green / Can Be Customized | Corrosion Integrity: | Excellent |
| Steel Plates Thickness: | 3mm To 12mm , Depends On The Tank Structure | Chemical Resistance: | Excellent |
| Size Of Panel: | 2.4M * 1.2M | Easy To Clean: | Smooth, Glossy, Inert, Anti-adhesion |
| Highlight: | Biogas plant for POME conversion,POME wastewater treatment project,Biogas plant design Honduras |
||
Product Description
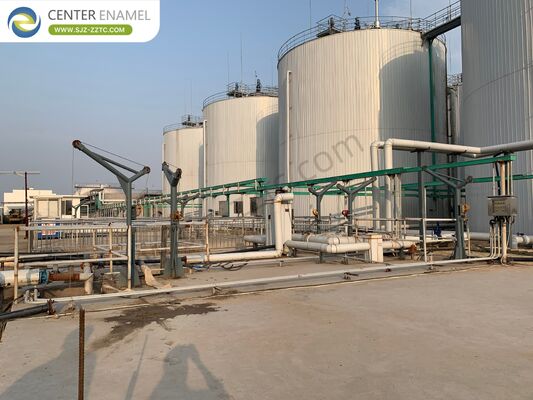
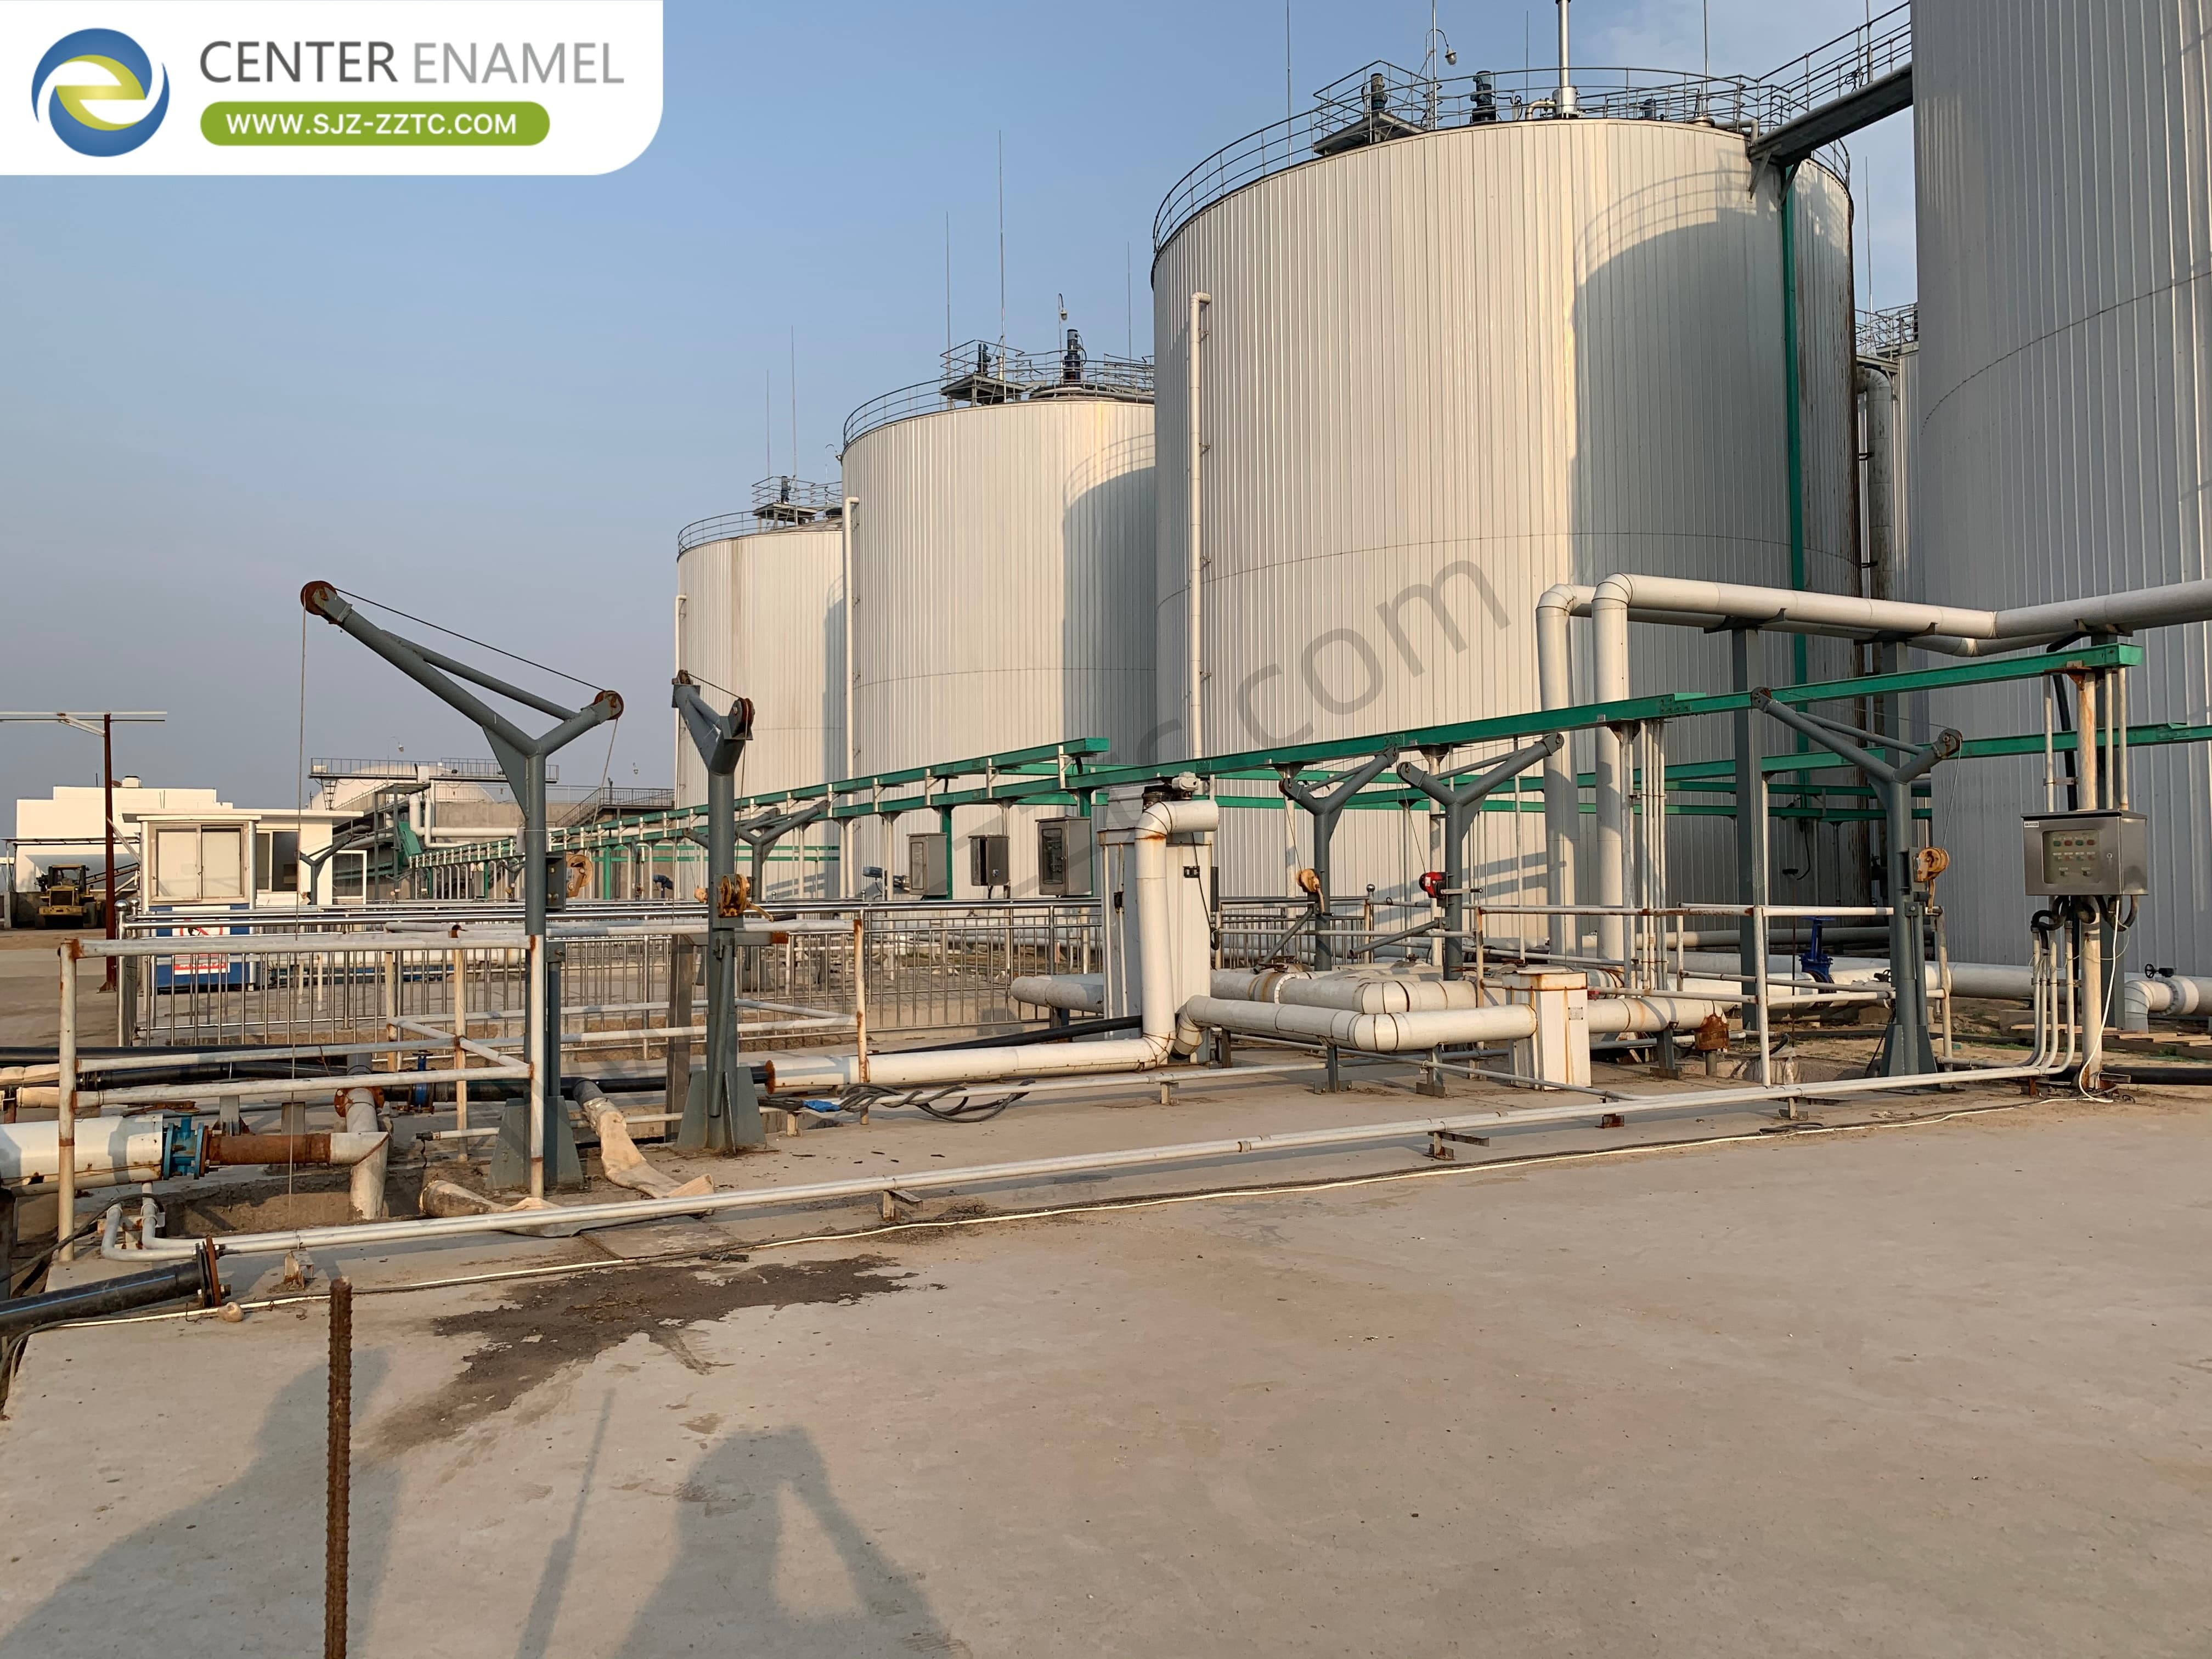
Practical Biogas Plant Design for Converting POME into Biogas in Honduras
Honduras is one of Central America’s emerging palm oil producers, and its mills are under growing scrutiny to manage palm oil mill effluent (POME) responsibly. This article explains how practical biogas plant design converts POME into biogas, from pretreatment and USR anaerobic digestion to biogas treatment, GFS tank storage, double membrane roofs, and auxiliary equipment. It also shows why Center Enamel’s integrated engineering, procurement, and construction model gives Honduran mills a single point of accountability for turning wastewater into clean, reliable energy.
Honduras’s POME Landscape and Treatment Pressures
Honduras is a significant palm oil producer in Central America, with plantations concentrated along the northern Caribbean coast and in the Sula Valley. Each tonne of fresh fruit bunches processed generates roughly 0.7–1 m³ of POME, a hot, acidic effluent with extremely high organic loading and oil content. Historically, many mills used open lagoon systems, which require large land areas and release methane directly into the atmosphere. Methane is a far more potent greenhouse gas than CO₂, and poorly managed lagoons can also contaminate soil and water bodies. Honduran environmental authorities are tightening discharge standards, while the palm oil sector’s sustainability commitments are pushing mills toward closed anaerobic digestion, where POME is converted into biogas for electricity, heat, and safer byproduct management.
The POME into Biogas Treatment Flow
Effective POME digestion begins with pretreatment that removes physical and chemical inhibitors. A mechanical bar screen intercepts large solids such as fibers, shells, and grit, preventing blockages and abrasion in downstream pumps and pipes. A horizontal flow oil separator then removes free fatty acids and grease, which can coat biomass granules and reduce methanogenic activity if allowed to enter the reactor. The pretreated wastewater enters a regulating tank designed to equalize flow, temperature, and pH, creating a stable feed for the anaerobic bacteria. This equalization step is particularly important in Honduras, where mill operations and seasonal rainfall can cause significant variability in POME quality and quantity. Once conditioned, the POME is pumped into the anaerobic reactor, where microorganisms convert organic carbon into biogas in the absence of oxygen.
USR Process for Reliable POME Digestion
The Upflow Solids Reactor (USR) is purpose-built for high-solids organic wastewater like POME, which typically contains 3–6% total solids. In the USR, feed is distributed across the tank bottom and flows upward through an expanded sludge bed. Anaerobic bacteria degrade the organic matter, and the resulting biogas rises to a gas holder at the top of the reactor. Treated effluent exits through a collection system near the top, while a recycle loop maintains the upflow velocity needed to keep the sludge bed active without washing out biomass. For mesophilic digestion of POME, the volumetric organic loading rate should be designed at 3–5 kg COD/(m³·d), a range that supports stable methane production while preventing acid accumulation. The USR’s vertical cylindrical design and airtight roof ensure reliable gas capture and long-term structural integrity.
Biogas Processing and Utilization
The biogas produced in the USR is a mixture of methane, carbon dioxide, and trace contaminants, including hydrogen sulfide. Before use, the gas passes through a dehydration unit that condenses and removes water vapor, followed by a desulfurization vessel containing media that adsorbs H₂S. A booster fan then pressurizes the cleaned gas, and a flowmeter monitors production. Clean biogas can fuel a biogas generator to produce electricity and heat for the mill, fire a boiler to supply hot water or steam for processing, or be flared safely during maintenance periods. Utilizing this gas displaces fossil fuels, reduces operational costs, and avoids the release of methane into the atmosphere.
GFS Tanks and Double Membrane Roofs for Biogas Systems
Glass-Fused-to-Steel (GFS) tanks and double membrane roofs are the two primary products in Center Enamel’s biogas infrastructure portfolio. GFS tanks are produced by firing glass particles onto steel panels at 820–930°C, creating a vitreous, non-porous coating that resists corrosion from hydrogen sulfide, organic acids, and fluctuating pH. This technology delivers a long service life and is widely used for anaerobic digesters and wastewater storage in bio-energy applications. The double membrane roof is the standard recommendation for most biogas projects. Its inner membrane stores biogas directly above the digester, eliminating the need for a separate gas holder, while the outer membrane protects against rain and wind. This integrated design reduces material and foundation costs and significantly reduces the plant’s footprint.
Diverse Storage Tank Options
Center Enamel supplies multiple tank configurations to suit different process streams and site requirements. Galvanized steel tanks offer a wear-resistant, durable coating for applications where moderate corrosion protection is sufficient. Fusion Bonded Epoxy (FBE) tanks, developed in partnership with AkzoNobel, provide advanced coating technology for enhanced chemical resistance and extended service life. Stainless steel tanks in AISI 304/316 are available for high-purity water storage or extremely harsh environments where glass and epoxy coatings may be unsuitable. This range allows Honduran mills to select the most cost-effective and technically appropriate tank for each stage of their biogas project.
Auxiliary Equipment for Complete Biogas Plants
A well-designed biogas plant includes equipment that ensures safe gas handling and efficient byproduct management. A gas holder provides buffer storage to balance gas production against utilization demand. A black membrane lagoon contains liquid digestate safely, preventing leachate from contaminating soil and groundwater. A hot water boiler can burn biogas to supply process heat, while an emergency torch safely destroys excess gas during upset conditions. Lifting pumps transfer POME and sludge reliably between stages. Dehydration and desulfurization tanks house the media that clean the gas. A screw sludge dewatering machine separates digested sludge into a solid fraction suitable for land application and a liquid fraction returned to the lagoon or used as liquid fertilizer.
Why Center Enamel Is the Right Biogas Plant Design Partner
Center Enamel’s strength lies in delivering complete, integrated biogas solutions rather than piecemeal equipment. As a biogas plant design and build partner, the company manages process design, equipment manufacturing, civil works coordination, installation, and commissioning under a single contract, removing the coordination risks and schedule delays common in multi-vendor projects. The USR reactor and GFS tank technologies are designed and manufactured in-house, ensuring that every component—from tank panels to gas holders—works together as a unified system. Certifications including CE/EN1090, ISO9001, NSF61, WARS, and EN28765, along with compliance with AWWA D103, OSHA, and EuroCode, demonstrate the company’s commitment to international quality standards. For Honduran palm oil mills, this integrated capability means faster project delivery, predictable performance, and a single point of accountability throughout the plant lifecycle.
Conclusion
Honduras’s palm oil industry has both an obligation and an opportunity: to manage POME responsibly while recovering its energy value. Anaerobic digestion through the USR process, supported by GFS tanks, double membrane roofs, and complete auxiliary equipment, provides a proven pathway to convert this high-strength wastewater into biogas for on-site power and heat. By partnering with a biogas plant design expert that offers end-to-end capability, Honduran mills can achieve regulatory compliance, reduce operating costs, and contribute to the sustainability of one of the nation’s most important agricultural industries.
FAQ
What makes POME suitable for anaerobic digestion?
POME is rich in biodegradable organic matter with high COD and BOD, and it is produced at warm temperatures. These characteristics create ideal conditions for anaerobic bacteria to break down the waste and produce methane-rich biogas without additional heating in tropical climates.
How long does it take to build a POME biogas plant?
Project timelines vary with capacity, site conditions, and scope, but a typical mill-scale biogas plant can be designed, manufactured, and commissioned within 6 to 12 months. Modular GFS tank construction and factory-controlled panel production help shorten on-site work.
What happens to the digestate after biogas extraction?
Digested POME retains valuable nutrients including nitrogen, phosphorus, and potassium. After dewatering, the solid fraction can be composted or applied to plantations, while the liquid fraction can be used as organic fertilizer or further treated before discharge.