-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (652)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (341)
-
Anaerobic Digester (202)
-
Industrial Water Tanks (349)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1692)
-
Double Membrane Roof (223)
|
What Is a Process Intensification Reactor? Principles, Technologies & Applications
| Place of Origin: | China |
| Brand Name: | Center Enamel |
| Certification: | ISO 9001,CE, NSF/ANSI 61, WRAS, ISO 28765, LFGB, BSCI, ISO 45001 |
| Minimum Order Quantity: | 1 Sets |
| Price: | 2000 |
| Delivery Time: | 2 months |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 200 sets / days |
|
Detail Information |
|||
Product Description
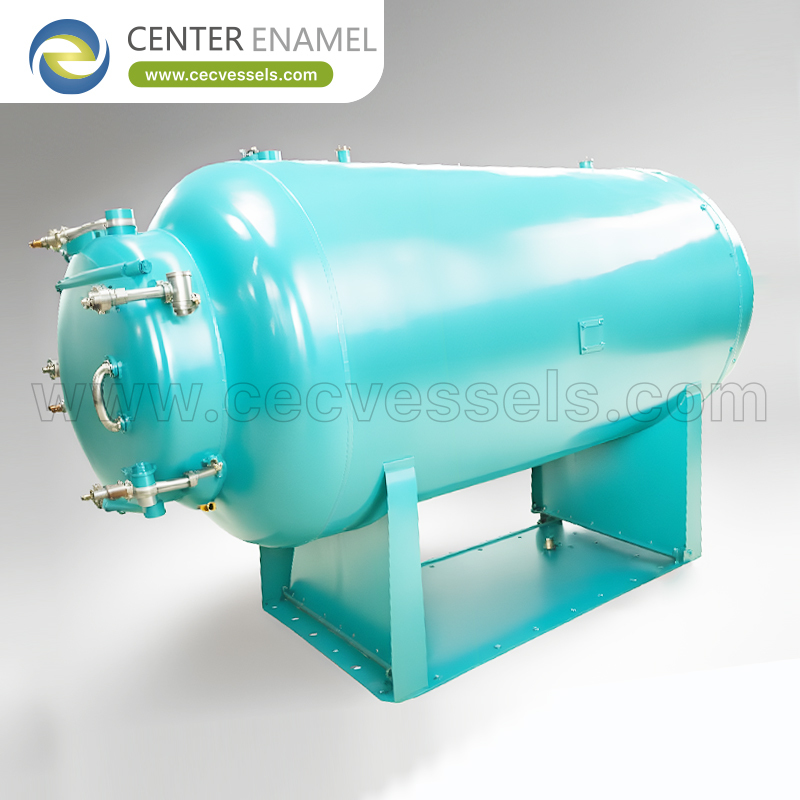
Answering the core question: What is a process intensification reactor, and how does it achieve order-of-magnitude improvements in productivity and safety? A process intensification reactor is an engineered system that achieves dramatic—typically 10 to 100-fold—improvements in reaction rate, selectivity, heat transfer, or mass transfer per unit volume compared to conventional stirred-tank reactors. By exploiting enhanced mixing, micro-scale heat transfer, high surface-area-to-volume ratios, and alternative energy fields (ultrasound, microwave, photochemistry), process intensification (PI) reactors reduce equipment size by 10–100*, improve intrinsic safety by minimizing reactive inventory, and enable reactions that are impossible or unsafe in conventional equipment.
- **Extreme Surface-to-Volume Ratio** Conventional batch reactors have S/V ratios of 30–100 m²/m³. Microchannel PI reactors achieve 10,000–50,000 m²/m³, enabling heat transfer coefficients of 1,000–20,000 W/m²·K (vs. 300–800 W/m²·K for jacketed batch). This allows isothermal operation of highly exothermic reactions such as nitration (heat release 150 kJ/mol) at reaction rates 10–100* faster than batch.
- **Enhanced Mass Transfer via Active Mixing** PI reactors use dynamic mixing mechanisms—oscillatory flow, spinning discs, or static mixers—to break down phase boundaries and reduce diffusion path lengths. Oscillatory baffled reactors (OBR) superimpose oscillatory motion on net flow, achieving mixing intensities equivalent to 10–20 CSTRs in series within a single tube, enabling plug-flow behavior at very low net flow rates.
- **Alternative Energy Field Integration** PI reactors can integrate non-thermal energy inputs: ultrasound (20–100 kHz) generates cavitation bubbles that collapse at 5,000°C and 1,000 bar locally, enhancing reaction rates by 2–10*. Microwave (2.45 GHz) provides volumetric heating with 5–10* faster energy transfer than conductive heating. Photochemical reactors use LED arrays at specific wavelengths to drive reactions with quantum yields of 0.1–1.0 without thermal activation energy.
- **Microchannel Reactor** A stack of etched or machined plates with internal channel diameters of 100–1,000 µm. The small channels achieve laminar flow with diffusion-controlled mixing in 1–100 milliseconds and heat removal rates of 10–100 kW/L. Used for hazardous reactions (fluorination, diazotization, peroxide synthesis) with inventory as low as 0.1–10 mL per channel, reducing explosion risk by 1,000* compared to equivalent batch processes.
- **Spinning Disc Reactor (SDR)** A rotating disc (500–3,000 rpm) on which liquid feed is spread into a thin film (50–200 µm thickness). The centrifugal force generates intense shear and renewal of the liquid surface, achieving mass transfer coefficients of 0.01–0.1 m/s and heat transfer coefficients of 5,000–30,000 W/m²·K. Primarily used for fast reactions, polymerization, and crystallization requiring high heat removal rates.
- **Oscillatory Baffled Reactor (OBR)** A tubular vessel containing periodic orifice baffles, with fluid oscillation superimposed on the net flow. The oscillation generates vortex mixing behind each baffle, achieving plug-flow behavior at low net flow rates (Re < 100). This decouples mixing from throughput, allowing long residence times (hours) in plug-flow mode without the impractical length required for conventional tubular reactors. Used for continuous crystallization, fermentation, and slow organic synthesis.
PI Reactor Type |
Enhancement Mechanism |
S/V Ratio |
Primary Application |
Microchannel |
Sub-millimeter channels |
10,000–50,000 m²/m³ |
Hazardous chemistry, nanoscale particles |
Spinning Disc |
Centrifugal thin film |
2,000–10,000 m²/m³ |
Fast reactions, polymerization, crystallization |
Oscillatory Baffled |
Oscillatory vortex mixing |
500–2,000 m²/m³ |
Long-residence plug flow, crystallization |
What is the primary benefit of process intensification over conventional reactor design?
Process intensification achieves 10–100* improvement in productivity per unit volume, enabling smaller, safer, and more energy-efficient plants. The reduced reactive inventory (often 1/100th to 1/1,000th of conventional) inherently improves safety—the worst-case runaway scenario releases far less energy. Capital costs are reduced by 30–70% due to smaller equipment, smaller footprint, and reduced safety systems.
What types of reactions benefit most from microchannel reactors?
Highly exothermic reactions (nitration, fluorination, diazotization, peroxide formation), reactions with hazardous intermediates (phosgene, diazomethane, hydrogen cyanide), and photochemical reactions requiring uniform light penetration. These reactions are either unsafe or impractical in batch reactors due to heat removal limitations and explosion risk.
How does a spinning disc reactor achieve such high heat transfer rates?
The rotating disc spreads liquid into a thin film (50–200 µm) with high surface renewal rate. The film's thinness reduces thermal resistance to a few micrometers, and the centrifugal force continuously refreshes the surface. Heat transfer coefficients of 5,000–30,000 W/m²·K are achieved, compared to 300–800 W/m²·K in jacketed batch reactors—a 10–50* improvement.
Can process intensification reactors replace all batch reactors?
No. PI reactors are best suited for continuous, single-product processes with steady demand. They are less suitable for multi-product facilities requiring frequent changeovers, reactions involving solids or slurries (which clog microchannels), and very slow reactions requiring days of residence time. The pharmaceutical industry typically uses PI for hazardous intermediate synthesis while retaining batch reactors for final API crystallization and formulation.