-
Glass Fused To Steel Tanks (896)
-
Stainless Steel Tanks (434)
-
Fusion Bonded Epoxy Tanks (652)
-
Galvanized Steel Tanks (321)
-
Aluminum Dome Roofs (1336)
-
Wastewater Storage Tanks (280)
-
Welded Steel Tanks (457)
-
Pressure Vessels (426)
-
Anaerobic Digester (202)
-
Industrial Water Tanks (349)
-
Glass Lined Steel Tanks (180)
-
Bolted Steel Tanks (389)
-
Sludge Storage Tank (115)
-
Biogas Storage Tank (173)
-
Leachate Storage Tanks (133)
-
Agricultural Water Storage Tanks (179)
-
Fire Water Tank (166)
-
Grain Storage Silos (146)
-
Biogas Projects (424)
-
Wastewater Treatment Projects (1712)
-
Double Membrane Roof (223)

|
Reliable Biogas Solution Provider for Municipal Sludge into Biogas in Singapore
| Place of Origin: | China |
| Brand Name: | CEC TANKS |
| Certification: | ISO 9001:2008, AWWA D103 , OSHA , BSCI |
| Model Number: | W |
| Minimum Order Quantity: | 1set |
| Price: | $5000~$20000 one set |
| Packaging Details: | PE poly-foam between each two steel plates ; wooden pallet and wooden |
| Delivery Time: | 10-30 days after deposit received |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 60 sets per month |
|
Detail Information |
|||
| Place of Origin | China | Brand Name | CEC TANKS |
|---|---|---|---|
| Certification | ISO 9001:2008, AWWA D103 , OSHA , BSCI | Model Number | W |
| Tank Body Color: | Dark Green / Can Be Customized | Corrosion Integrity: | Excellent |
| Steel Plates Thickness: | 3mm To 12mm , Depends On The Tank Structure | Chemical Resistance: | Excellent |
| Size Of Panel: | 2.4M * 1.2M | Easy To Clean: | Smooth, Glossy, Inert, Anti-adhesion |
| Highlight: | municipal sludge biogas solution,biogas project Singapore,wastewater treatment biogas system |
||
Product Description
Singapore treats almost all its used water through the national water agency's water reclamation plants, and every cubic metre produces a concentrated wet sludge that must be stabilised before disposal. With limited land and a national push for energy self-sufficiency in water operations, turning municipal sludge into biogas is no longer optional. This guide explains how a turnkey project—built around GFS tanks, a CSTR digester, and a double membrane roof—captures methane from sewage sludge, reduces waste-to-energy loads, and gives Singaporean operators a reliable biogas supply for on-site power and heat.
Singapore's used water is collected and treated at water reclamation plants spanning Tuas, Changi, Kranji, Ulu Pandan, and Seletar. Secondary treatment generates both primary sludge and waste activated sludge, which are thickened, conditioned, and dewatered before leaving the plant. Because Singapore has virtually no land for lagoons or agricultural spreading, the conventional route has long been to truck dewatered sludge to waste-to-energy plants for incineration, with the resulting ash shipped to Semakau Landfill. This chain is energy-intensive, transportation-heavy, and ultimately dependent on a finite landfill horizon. As plant throughputs rise with population and water demand, the volume of wet sludge continues to climb, pressing operators to recover energy from the sludge itself rather than burn it raw. Sludge stabilisation also cuts odour and pathogen load, a critical concern in a densely built city where treatment plants sit close to residential and commercial districts.
Converting municipal sludge into biogas through anaerobic digestion delivers three core advantages. First, it stabilises the sludge, reducing volatile solids, odour, and pathogens so that the dewatered cake is easier and safer to handle. Second, it captures methane that would otherwise be lost during incineration or landfill decay, and uses it to offset the electricity and heat demand of the treatment plant. Third, it cuts the mass going to incineration, lowering transport costs and ash volumes. The typical process flow begins with thickening and dewatering of mixed sludge, followed by homogenisation in a balance tank that equalises flow and solids content. The conditioned sludge is then pumped into a heated anaerobic digester. After digestion, the stabilised slurry passes through a buffer tank and a mechanical dewatering step, and the separated liquor returns to the water treatment stream while the digested cake is sent for final disposal or beneficial reuse.
The Continuous Stirred-Tank Reactor (CSTR) is the workhorse of municipal sludge digestion. CSTR is an anaerobic treatment technology in which fermentation feedstock and microorganisms are fully mixed inside a closed, insulated tank. The reactor is equipped with a mechanical stirring device—an agitator shaft, paddles, and a top-entry drive— that keeps the viscous, solids-laden sludge homogeneous, prevents stratification, and maintains uniform temperature. By feeding semi-continuously at a controlled mesophilic or thermophilic temperature, the sludge and the anaerobic microbial community remain in a well-mixed fermentation state that effectively breaks down organic matter. The digester also carries a dedicated biogas pipeline, a feed inlet, a sludge discharge point, and a positive and negative pressure protector that safeguards the vessel against over-pressure or vacuum swings as gas is withdrawn.
Raw biogas leaving the digester is saturated with moisture and contains hydrogen sulfide, both of which damage engines, boilers, and pipelines. The treatment train therefore starts with biogas dehydration to remove free water, followed by desulfurisation to reduce sulfur compounds. A booster fan delivers the conditioned gas at a steady pressure through a flowmeter to the chosen end use. The four common utilisation pathways are: biogas generation, where the methane drives a generator to offset plant electricity; a boiler, where the gas is combusted directly to heat digesters or buildings; a flare system, which provides safe pressure relief when gas production exceeds on-site demand; and compressed natural gas upgrading, where the gas is purified to over 95% methane and compressed for injection or vehicle fuel.
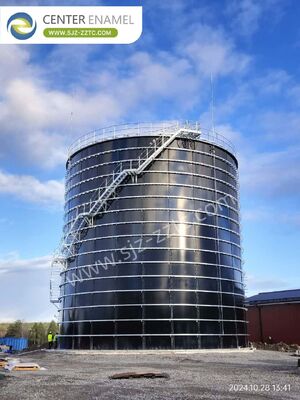
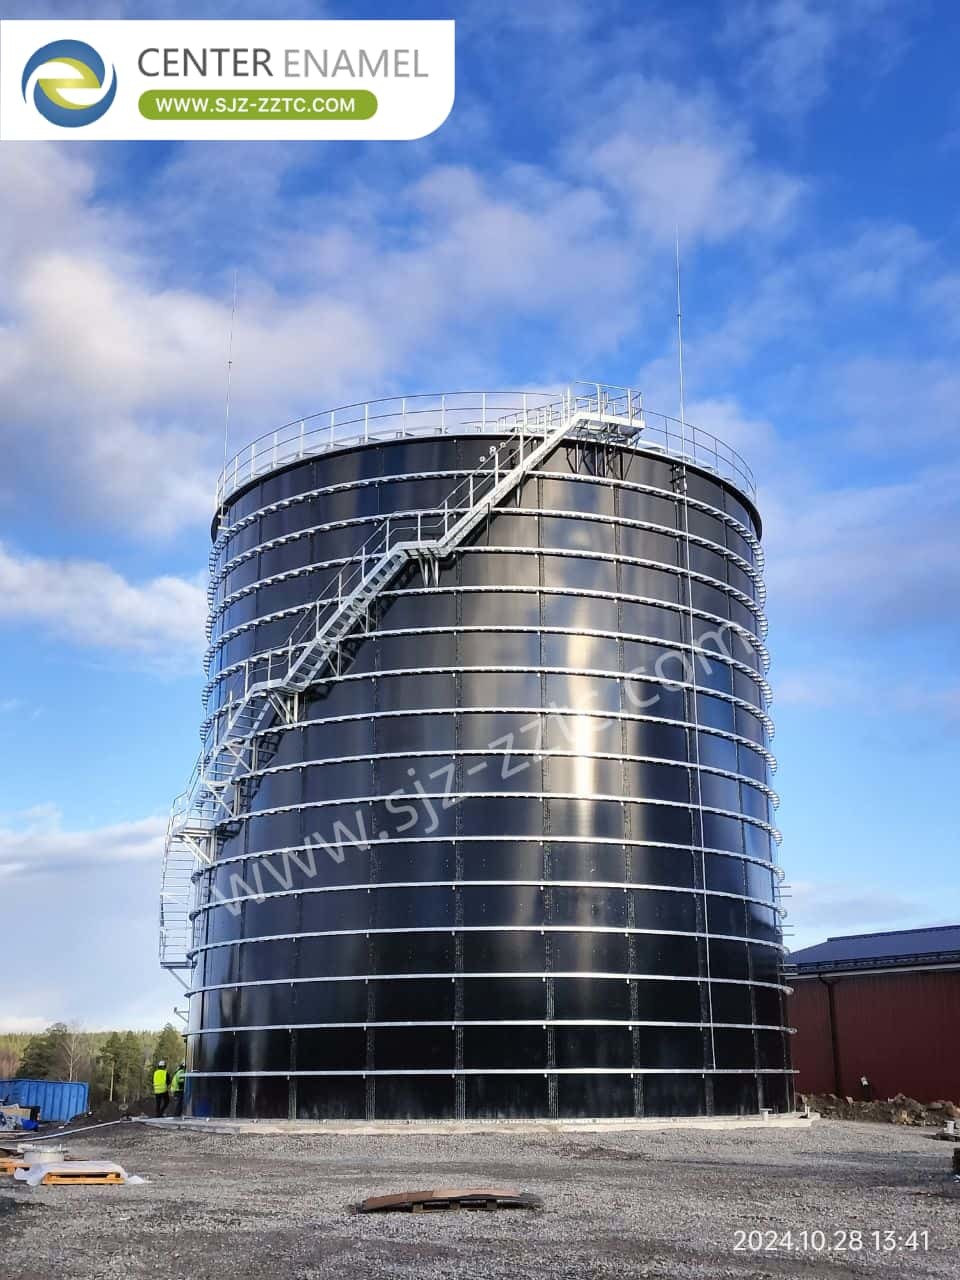
Two products define a modern sludge-to-biogas plant. The first is the Glass-Fused-to-Steel (GFS) tank. After firing at 820 °C–930 °C, molten glass reacts with the steel plate surface to form an inert, inorganic bond that combines the strength and flexibility of steel with outstanding corrosion resistance. The double coating layer structure (2C2F) applies distinct interior and exterior ground and surface coatings, giving robust protection against the hydrogen sulfide, condensate, and humid air found inside a covered digester. The second product is the double membrane roof, which serves as both the tank cover and the integrated gas holder. Under normal working conditions it is the preferred solution: it directly reduces roof cost, and compared with a separate ground-mounted gas holder it significantly reduces the floor area—a decisive advantage on the compact plots typical of Singapore's water reclamation plants.
Center Enamel matches tank material to each duty in the sludge treatment train:
Glass Fused To Steel (GFS) tanks: flagship digesters, buffer tanks, and filtrate storage tanks, backed by the 2C2F dual-coating system and international certifications.
Galvanized Steel Tanks: receive a tough, wear-resistant, durable protective coating for general water and filtrate equalisation service.
Fusion Bonded Epoxy (FBE) tanks: developed with a global coatings partner for a bonded epoxy finish on moderately corrosive streams.
Stainless Steel Tanks: in AISI 304/316, reserved for high-purity water, chemical dosing, and the most corrosive process duties.
A turnkey sludge digestion project depends on supporting hardware as much as on the digester itself:
Gas Holder stores conditioned biogas and smooths peaks between digester output and engine or boiler demand.
Black Membrane covers filtrate or sludge storage lagoons and prevents fugitive emissions on expansion stages.
Solid-liquid Separator dewaters digested slurry, producing a manageable cake and a separated liquor stream.
Torch System safely flares start-up or excess gas when downstream equipment is offline.
Lifting Pump transfers conditioned sludge and digested sludge between tanks without clogging.
Dehydration and Desulfurization Tank cleans raw biogas before it reaches engines or upgrading units.
Screw Sludge Dewatering Machine further reduces cake moisture for cheaper transport and final disposal.
Center Enamel acts as a single accountable biogas solution provider across the whole project lifecycle:
EPC service: one contract covers process design, equipment supply, installation supervision, and commissioning.
Process Package: a matched thickening, CSTR digestion, gas handling, and dewatering train sized to the plant's daily sludge tonnage.
Equipment Supply: GFS tanks, double membrane roofs, gas holders, separators, pumps, and dewatering machinery delivered under one schedule.
Certified construction: built under ISO 9001, with CE/EN1090, NSF61, WRAS, and EN28765 references and designs aligned to AWWA D103, OSHA, EN28765, and EuroCode.
Global scale: a 150,000 m² R&D and production base, 250,000 sheets per year capacity, 500+ employees, and references in more than 100 countries.
Dense-urban know-how: compact layouts, odour control, and corrosion-resistant finishes tuned to city-centre treatment plants.
For Singapore's water reclamation operators, municipal sludge is a concentrated organic resource sitting inside an energy-intensive process. A well-engineered anaerobic digestion project built around a CSTR digester, GFS tank, and double membrane roof captures methane that offsets plant electricity and heat, reduces the mass sent to incineration, and shrinks the footprint needed on a tightly planned site. With an experienced biogas solution provider, Singaporean operators can move further toward a self-sufficient water-recycling system.
Q1: How much biogas can be produced from municipal sludge?
Typical digester gas yields range from 0.6 to 1.1 m³ per kilogram of volatile solids destroyed, depending on sludge blend, retention time, and digestion temperature. The gas usually contains 60–65% methane.
Q2: What is the difference between mesophilic and thermophilic digestion? Mesophilic digestion runs at about 35 °C with a longer retention time and lower energy input; thermophilic digestion runs at about 55 °C with faster pathogen reduction and higher gas output, but requires more heating and closer process control.
Q3: Can digested sludge be used in land rehabilitation in Singapore?
In practice, land application is very limited in Singapore's urban context. Stabilised, dewatered cake is most commonly sent for co-disposal or beneficial use off-island, while the recovered biogas is used to offset the plant's own energy demand.